
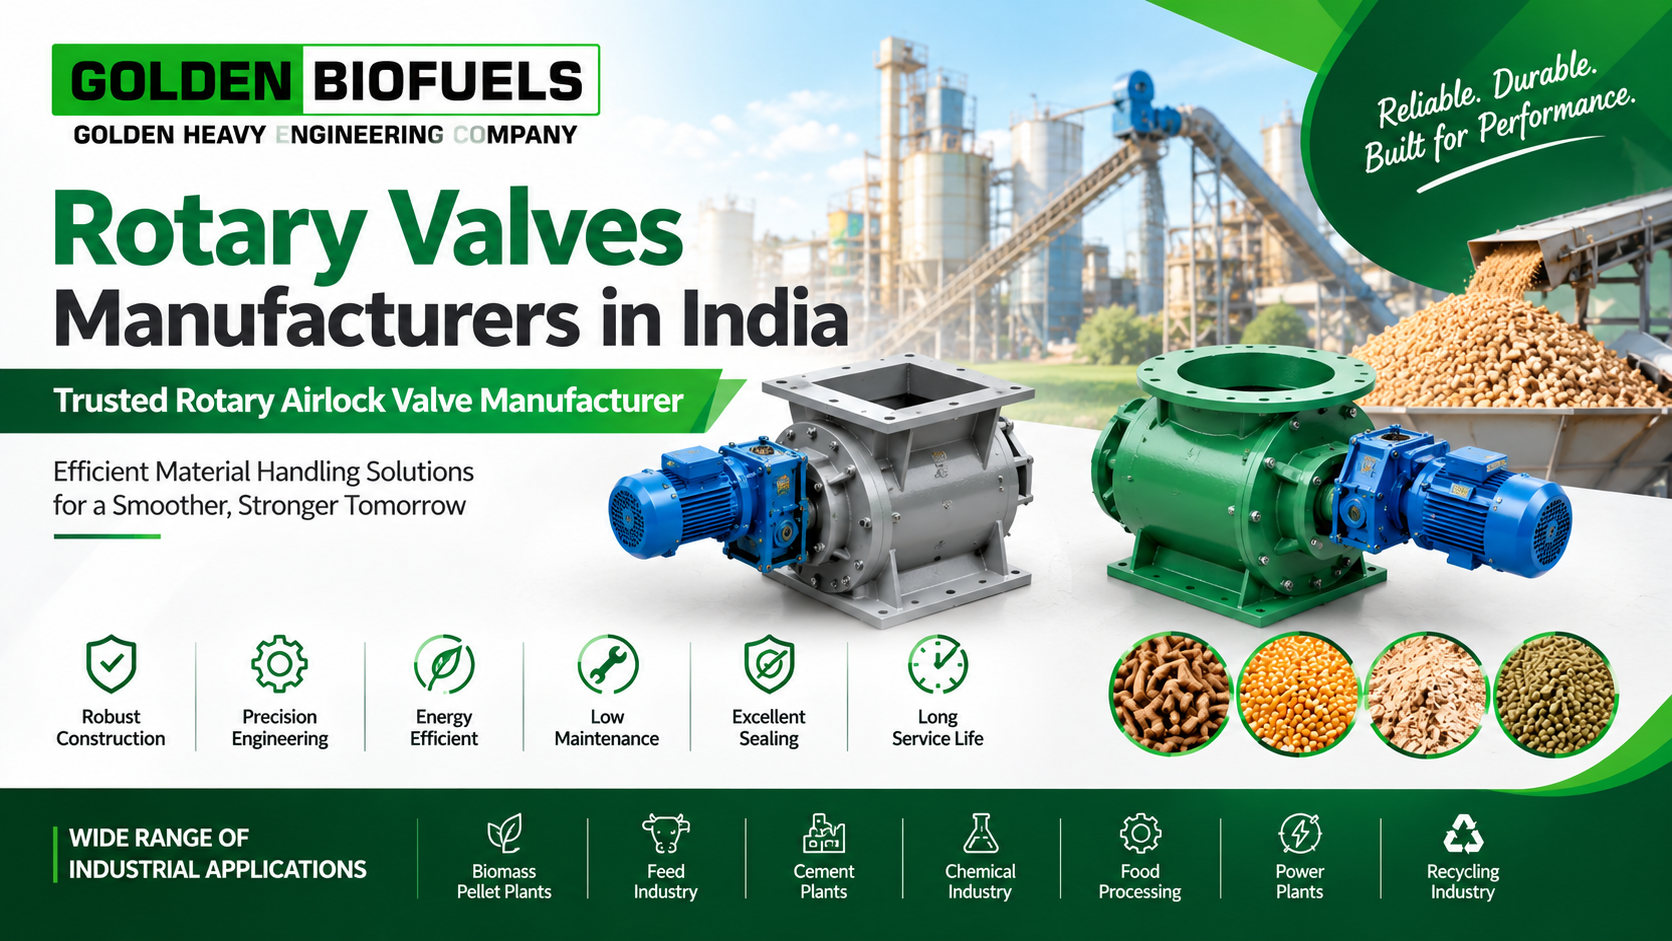
Efficient material handling is the main concern for any industry that deals with processing powders, pellets, granules, and other materials. A rotary valve is an essential component of a material handling system, which helps to control the material flow while protecting the system against air pressure loss.
Golden Biofuels is a reputed rotary valve manufacturer in India, providing high-end rotary airlock valves that ensure efficient functioning of industrial plants.
Our company’s rotary valves are engineered to perfection and manufactured using high-quality materials to offer enhanced productivity and reduced material wastage.
Whether you are engaged in biomass pellet manufacturing, feed milling, cement manufacturing, or chemical processing, Golden Biofuels is your one-stop solution for all your rotary valve needs.
Why Choose Golden Biofuels?
Golden Biofuels specializes in manufacturing equipment with high endurance, energy efficiency, and low maintenance. Our expertly designed industrial valves have been tested and proven to offer a higher level of performance.
The key features of our rotary valves are:
(1) Heavy-duty and sturdy
(2) Easy maintenance and exceptionally high tightness
(3) Low operating and maintenance costs
(4) High-performance and long-lasting
(5) Suitable for continuous industrial operations
(6) Available in a range of sizes and capacities
(7) Precision-engineered rotor mechanism
Our team of professional engineers can advise you on the most suitable option for your application. We strive to fully comprehend our client’s needs to be able to recommend the most appropriate configuration of a rotary valve.
Introduction to Rotary Airlock Valves
A rotary airlock valve is a mechanical device which allows free material flow while preventing air loss or ingress. It is commonly applied in pressure vessels, where a controlled amount of material must be transferred from one chamber to another. The rotary valve’s rotor rotates at a specific speed to ensure a continuous material flow from the inlet to the outlet.
The unique design of a rotary airlock valve enables it to continuously convey powder, pellets, or granules without depleting the pressure of a conveying system. The rotary valve’s simplicity in design offers an array of benefits in industrial material handling.
Overview of the Features of Rotary Valves Manufactured by Golden Biofuels
Golden Biofuels uses cutting-edge technologies while fabricating heavy-duty and highly efficient industrial valves. The unique design concepts and the use of modern machinery enable the production of high-performance equipment. Below are the key features of our rotary airlock valves:
High-performance and reliable
(1) Excellent dust-tight & leak-proof capability
(2) Superior wear resistance and corrosion resistance
(3) Smooth and vibration-free performance
(4) Lightweight yet heavy-duty
(5) Long service life
(6) Designed for continuous high-speed operation
(7) Easy maintenance and simple installation
We also offer a wide range of industrial valves, which can be applied for continuous and intermittent operations.
Industrial Applications of Rotary Valves
Rotary airlock valves have a broad range of applications. In fact, any industry, which uses a system for continuous material transfer or transportation can benefit from the enhanced performance of a rotary valve.
The major industrial applications of our rotary valves include:
(1) Biomass Pellet Plants
(2) Feed Mills
(3) Food Processing Units
(4) Cement Plants
(5) Chemical Industries
(6) Fertilizer Plants
Our high-performance rotary valves can be applied in powder conveying, granulation, and pelletizing systems. They are suitable for transporting a variety of materials like pellets, powders, grains, ash, sawdust, wood chips, and many others.
Key Benefits of Our Rotary Valves
The performance of a rotary airlock valve directly impacts the efficiency of an industrial plant. Therefore, it is essential to choose a high-quality valve, manufactured using the latest technologies and machinery. At Golden Biofuels, we offer rotary airlock valves that have been engineered to provide you with the following benefits:
(1) Enhanced efficiency and continuous material flow
(2) Improved overall productivity of your industrial plant
(3) Reduced material wastage and operational costs
(4) Higher degree of dust-proof and pressure-proof performance
(5) Longer service life and reduced maintenance needs
Our experienced and skilled professionals have been providing customers with high-performance equipment for a wide range of industrial applications. The superior quality and cost-effectiveness of our equipment have made us one of the most reputable Rotary Valves Manufacturers in India.
Customized Solutions for Your Industry
Each industrial facility has unique material handling needs, which should be addressed when choosing a rotary valve. The main factors to consider are the properties of the transported material, the size of the facility, and the required conveying capacity.
The expert team of our engineers can help you to choose the most suitable valve configuration for your application.
When choosing a rotary airlock valve, it is essential to consider the following factors:
(1) Valve mounting requirements
(2) Size and capacity
(3) Material of construction
(4) Drive arrangements
(5) Rotor design
Our professional experts can assist you with selecting the most suitable option for a wide range of industrial applications.
Uncompromising Quality to Ensure Your Full Satisfaction
At Golden Biofuels, we take the quality of our products very seriously. Our team of professional engineers uses modern machinery to ensure that our valves are able to meet the needs of a wide range of industries.
Every single component of our rotary airlock valves is engineered for long service life and continuous performance. As a result, our valves offer enhanced plant productivity and reduced maintenance costs.
Why are Rotary Airlock Valves Important?
An appropriately selected rotary airlock valve can enhance the performance and efficiency of an industrial plant. A high-quality valve ensures uninterrupted material flow, minimises pressure loss, and prevents material wastage. Moreover, the enhanced dust-proof performance of a rotary valve ensures efficient bagging and dust collection.
Our company can help you to select the most appropriate option, depending on the type of material you need to convey, its properties, and your plant’s requirements. Choosing the right equipment manufacturer is essential if you want to enhance the efficiency of your industrial plant and reduce maintenance costs.
Golden Biofuels is a reliable rotary valve manufacturing company with the necessary expertise to fulfill all your material handling needs.
Whether you are looking for a standard rotary airlock valve or a customized solution, we will provide you with rotary valves, designed for continuous high-speed operations.
Our professional engineers offer expert advice on the most suitable equipment for your industrial application. The superior performance and enhanced reliability of our equipment make us one of the most reputable Rotary Valves Manufacturers in India.
Summary
When searching for a reliable Rotary Valves Manufacturers in India or a Rotary Airlock Valve Manufacturer, you should consider contacting Golden Biofuels, which has been offering high-quality industrial products for a wide range of industries. Our company provides high-performance rotary airlock valves, manufactured using the latest technologies to ensure enhanced product quality and performance.
Our expert team can advise you on the most suitable equipment option for your industrial application. We offer cost-effective and reliable solutions for all your material handling needs.
Frequently Asked Questions (FAQs)
1. Why do you recommend Golden Biofuels as a rotary valve manufacturer?
Golden Biofuels offers a wide range of high-quality rotary valves, which utilize advanced engineering and manufacturing technologies to ensure prolonged service life and continuous operation.
2. What is the application of a rotary airlock valve?
A rotary airlock valve isolates the pressure vessel from the atmosphere while allowing free material flow.
3. What industries can benefit from the performance of Golden Biofuels rotary valves?
Our company provides rotary airlock valves for biomass pellet plants, feed mills, cement plants, food processing units, chemical industries, fertiliser plants, recycling industries, and power plants.
4. Can Golden Biofuels manufacture a customised rotary valve?
We can offer a wide range of customised solutions for all your industrial material handling needs.
5. What types of materials can be conveyed using our rotary valves?
Our valves are suitable for conveying powder, pellets, grains, sawdust, wood chips, ash, fertilisers, chemicals, cement, and a wide range of other materials.
6. Why are rotary valves from Golden Biofuels reliable and long-lasting?
Our rotary valves offer exceptional performance and can be applied in a wide range of continuous industrial operations. They utilize advanced engineering concepts and are manufactured using high-quality materials.